Stress Relieving
Stress Relieving
Dimensional Stability During & After Heavy Machining
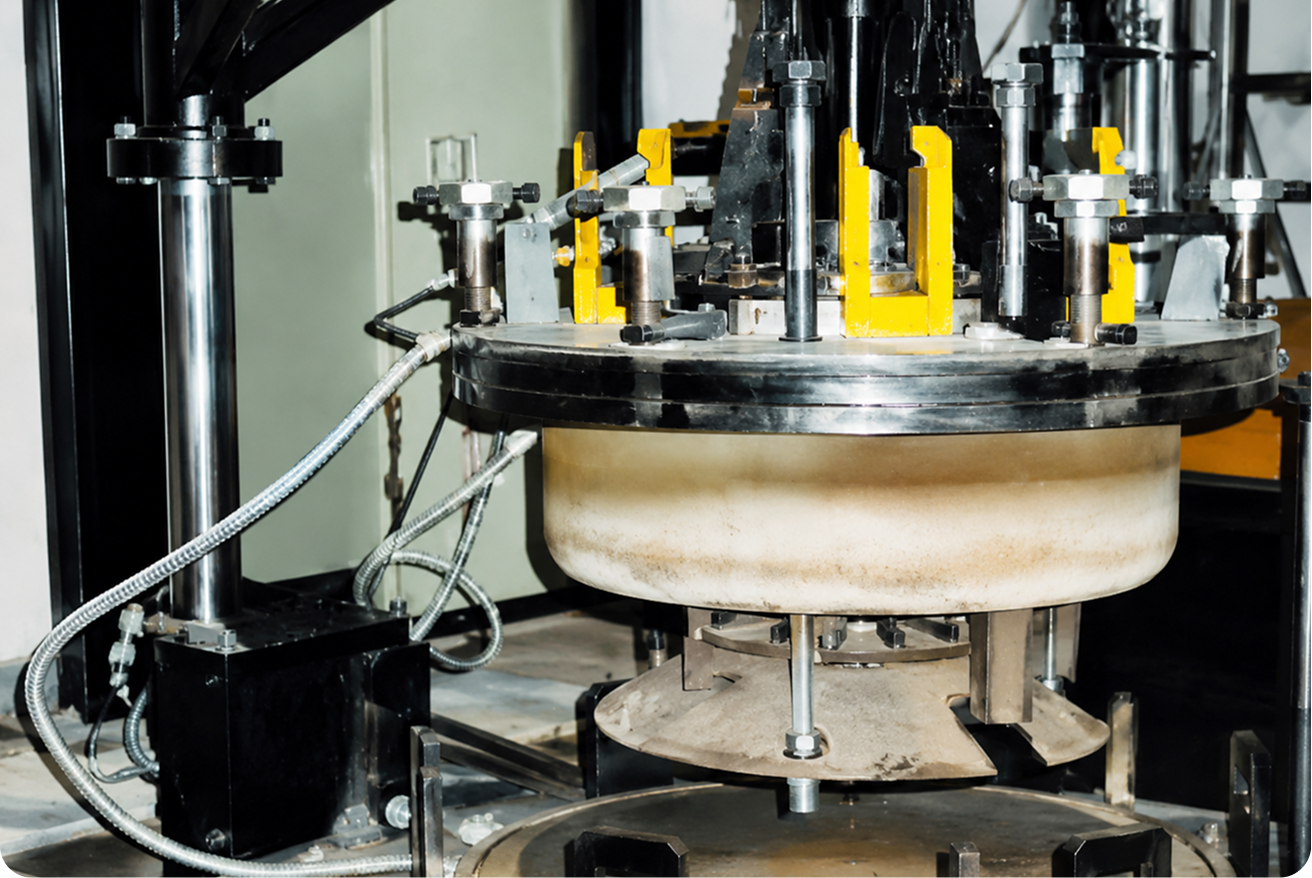
Stress relieving heats components below the critical transformation temperature (typically 550°C - 650°C) followed by uniform slow cooling to discharge residual stresses created by welding, heavy rough milling, cold forming, or EDM wire erosion.
Key Specifications
Prevents Warping, Cracking & Tolerances Drift
Without stress relieving, residual internal stresses gradually release over time or during finish machining, causing expensive parts to warp out of dimensional tolerance or crack in service.
Critical Stress-Relieving Use Cases
Used across aerospace tooling, large weldments, and complex EDM parts.
Complex Mould Bases & Plates
Rough-machined plastic mould cavities and core retainers before finishing.
Heavy Welded Machinery Bases
Robot arms, press frames, machine beds, and structural fabrications.
EDM Wire-Cut Blocks
Hardened tool steel blocks stress-relieved prior to wire-cutting to avoid splits.
Pressure Vessels & Piping
ASME Post-Weld Heat Treatment (PWHT) compliant stress relief.
Calibrated Chart Recording & Thermocouple Mapping
Digital multi-point time-temperature graph recording verifies uniform soak time throughout heavy cross-sections in compliance with international aerospace standards.
Other Heat Treatment Services
Vacuum Hardening
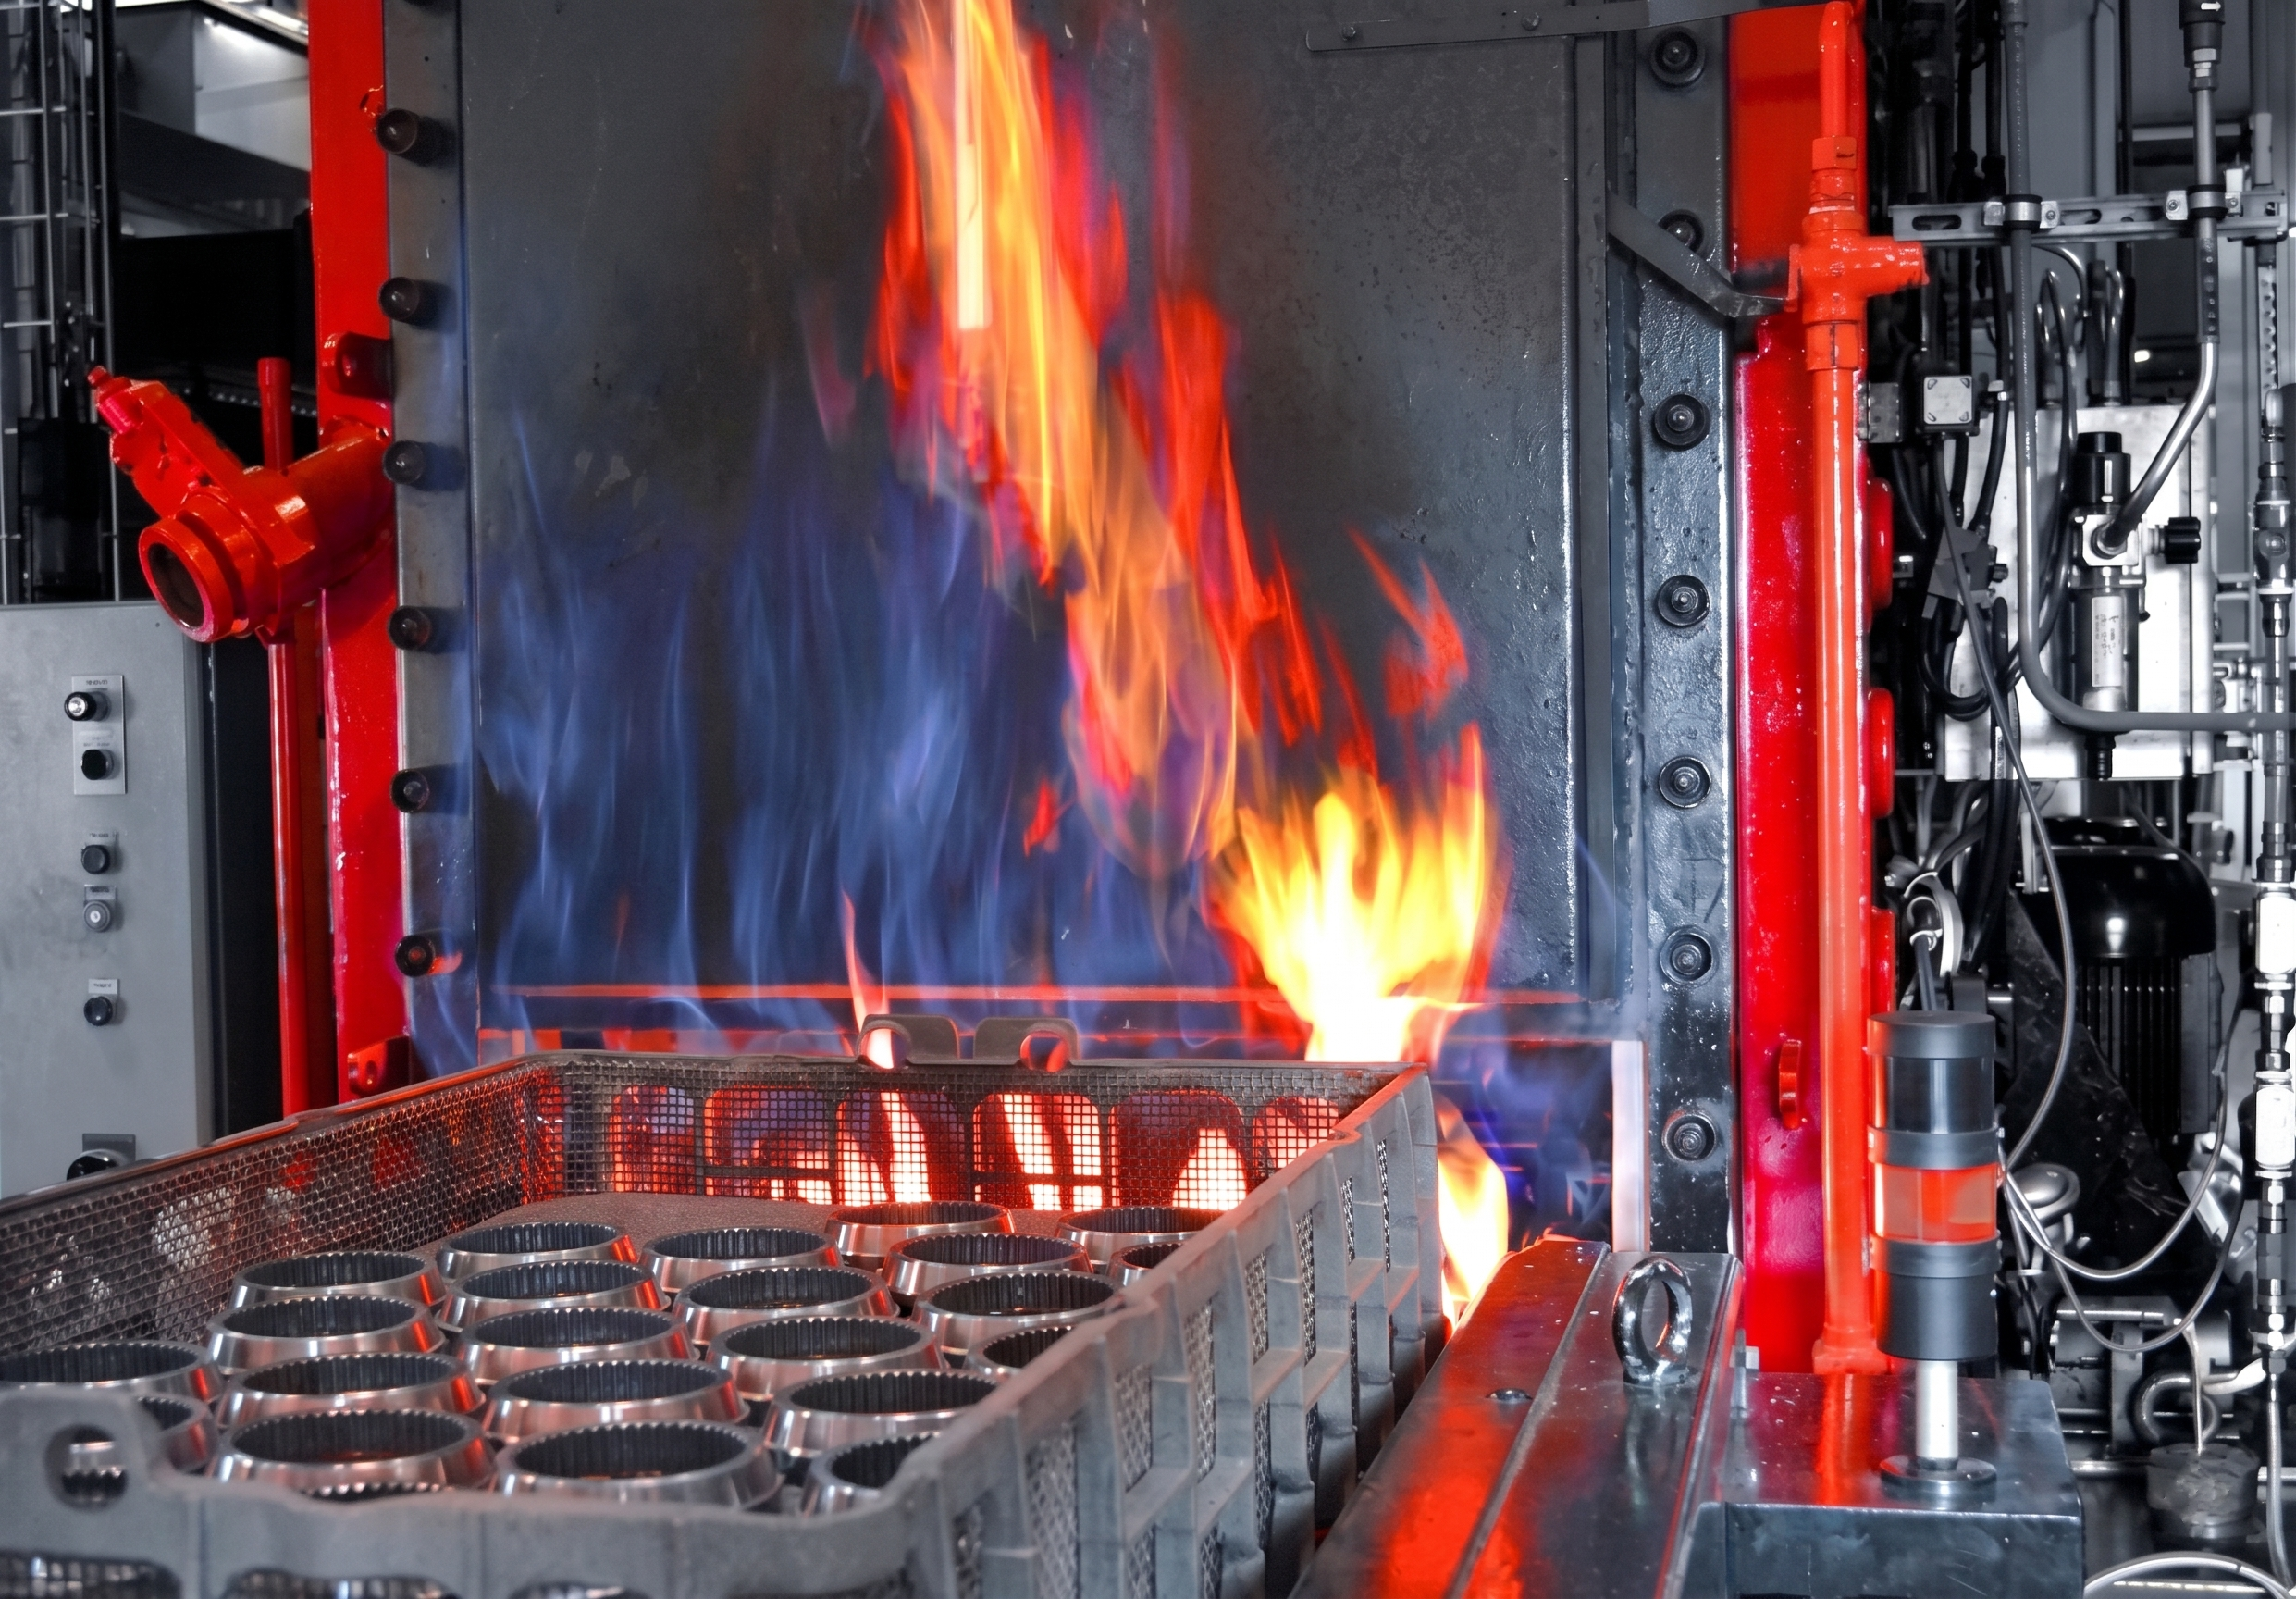
Delivers bright, oxidation-free hardening with minimal distortion.
Gas Carburising
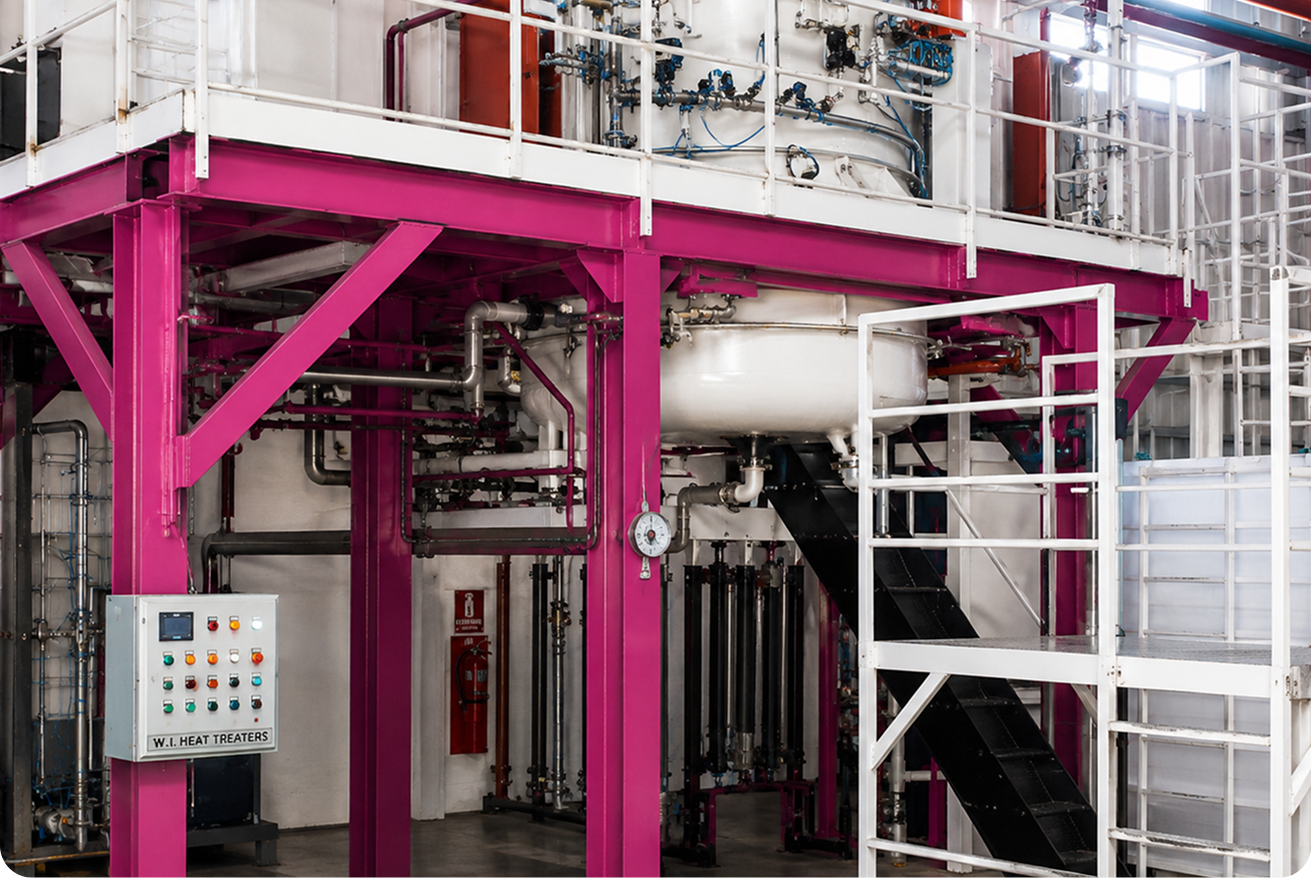
Enhances surface hardness while maintaining a tough core for improved durability.
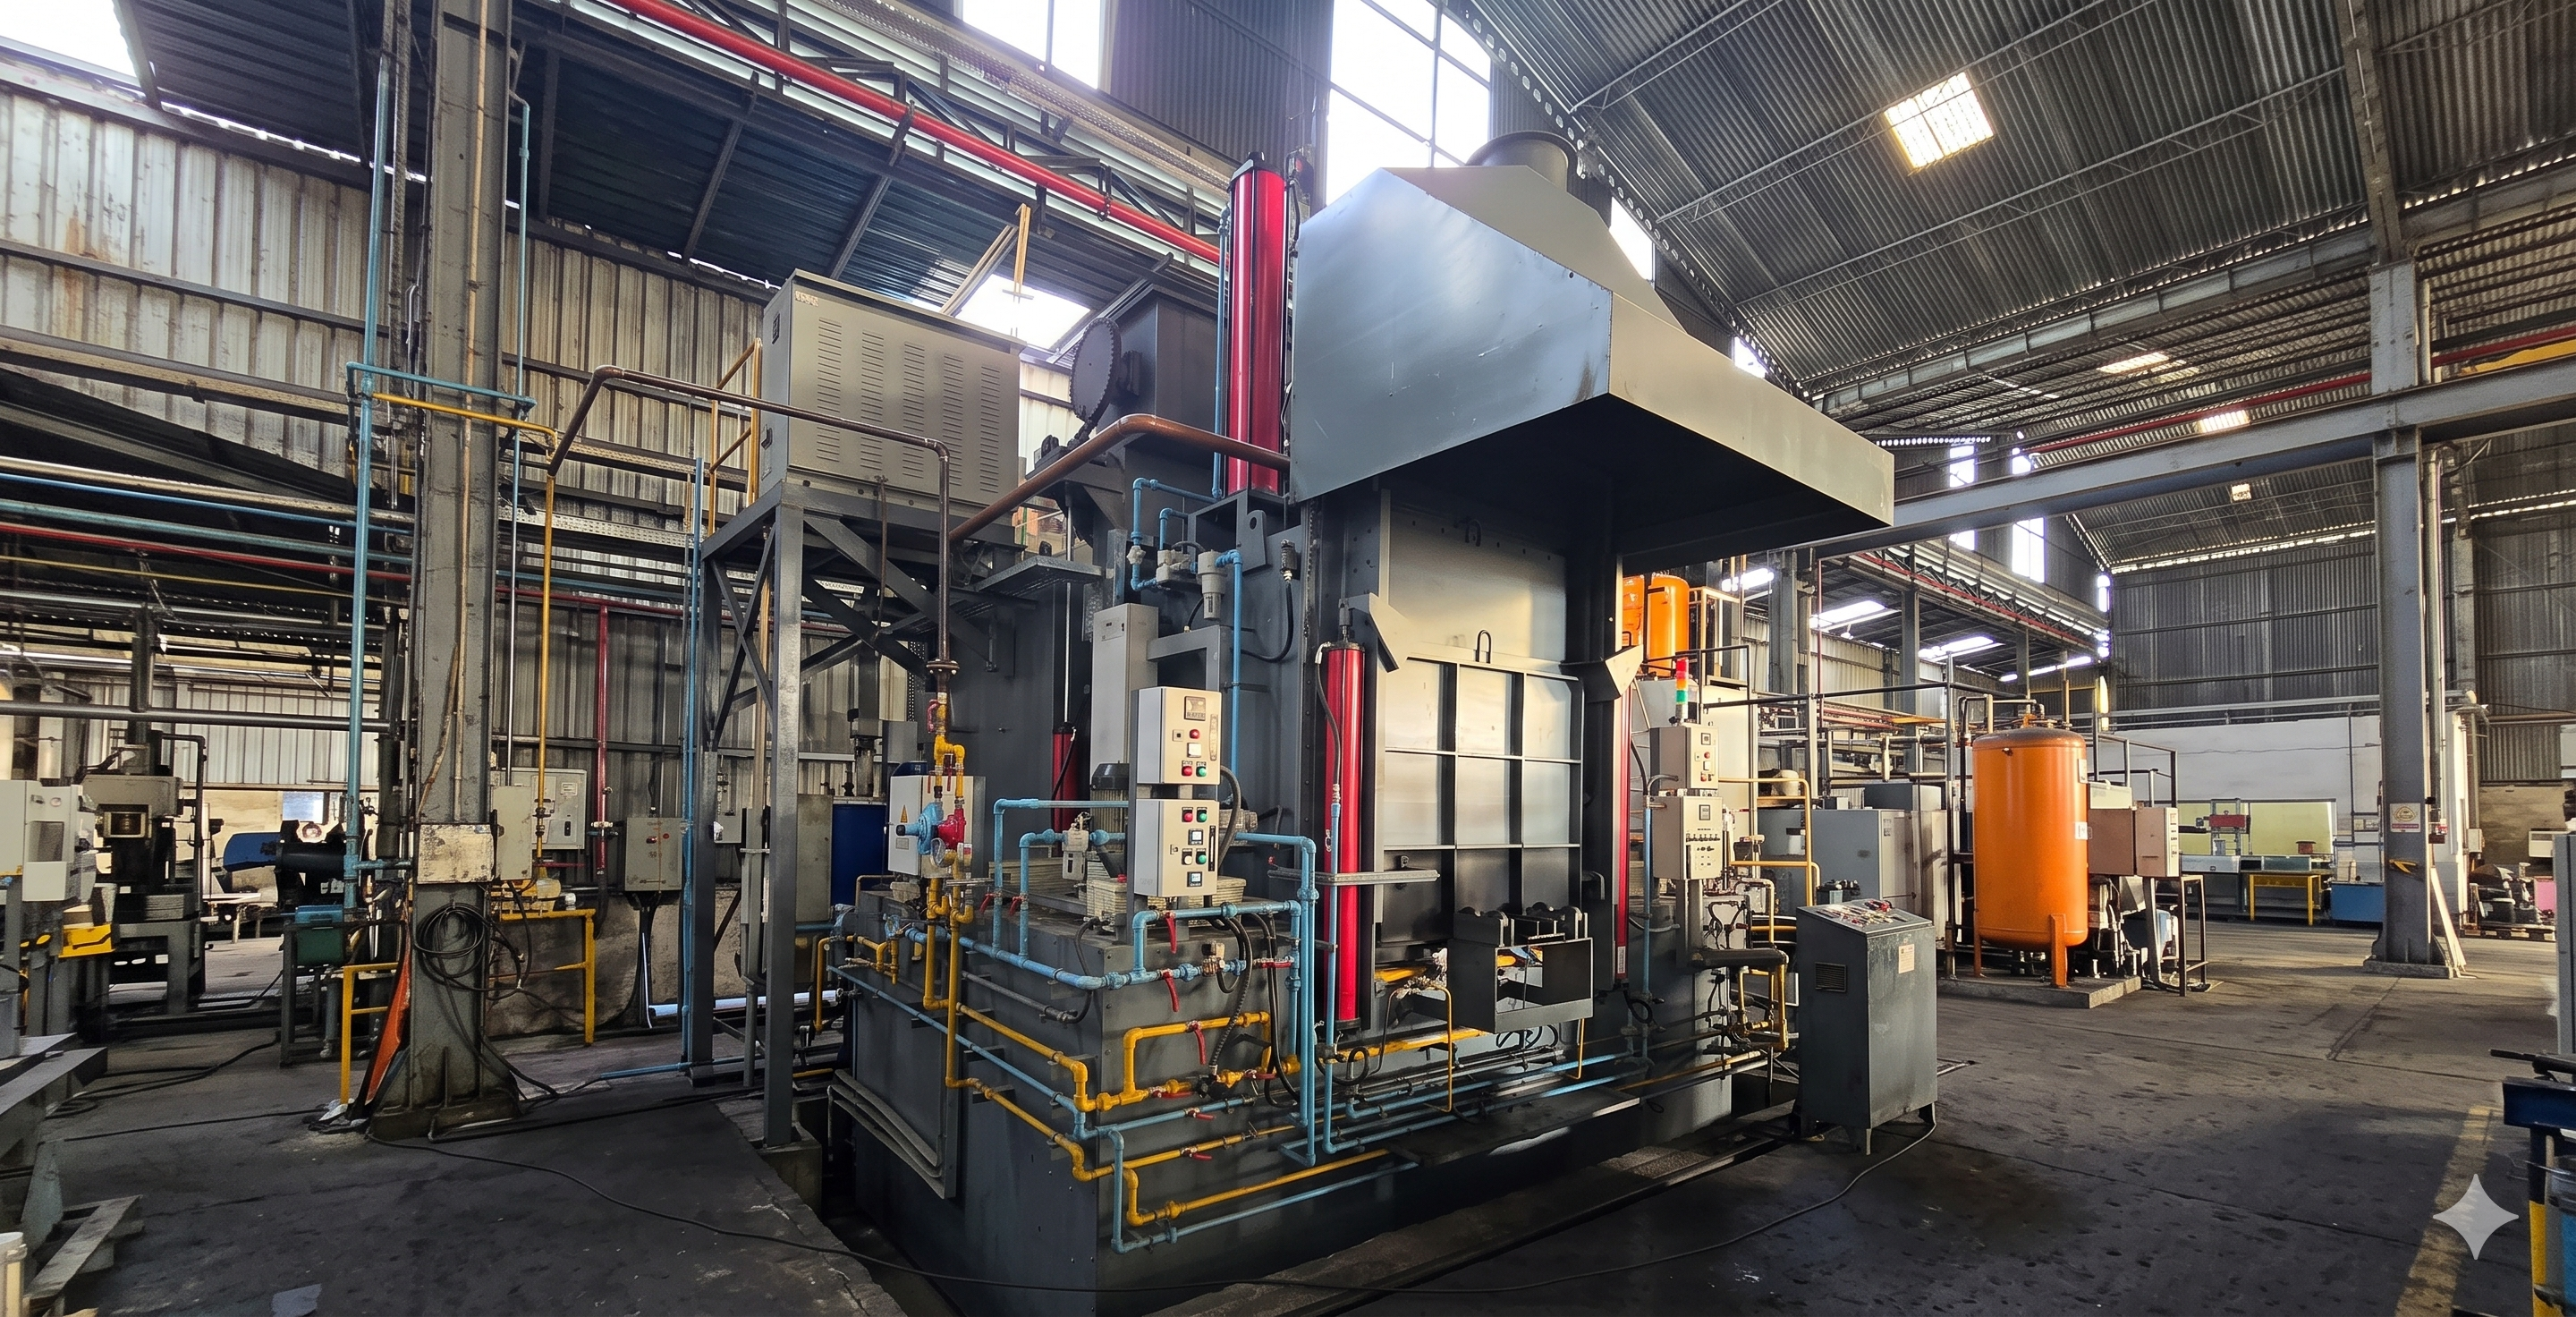
Gas Nitriding
Produces a hard, wear-resistant surface without compromising core strength.